Every week our engineering desk receives the same email: “Here is our STEP file — it is production-ready, we already had it molded in ABS.” Three weeks later the samples come back cracked at the handle root, the lid no longer fits, or the wall reads 3.1 mm instead of the intended 4.0 mm. Nothing was wrong with the CAD. What was wrong was the assumption that a 3D model optimized for injection molding or CNC machining can be dropped straight into a ceramic process.
Ceramic is not a polymer and not a metal. The body starts as a water-based clay mass, loses 6%–8% of its linear dimension while drying, then collapses a further 13%–15% as it vitrifies at 1310°C. It is formed inside a porous gypsum mold that must be opened by hand, it shrinks non-uniformly if wall sections are unbalanced, and it will tear itself apart if a thick section is locked between two thin ones. This guide is the DFM checklist we send to designers before a single mold is cut — written from the shop floor of a Dehua source factory, not from a textbook.
1. The Four Failure Modes of “Injection-Molding-Ready” CAD in Ceramics
Before correcting geometry, understand what actually breaks:
- Kiln distortion (warp & sag). Uneven wall thickness creates differential shrinkage. A 9 mm base under a 3 mm rim will pull the floor into a bowl shape during vitrification. Ceramic has no packing pressure to hold the shape — gravity and shrinkage do the shaping.
- Drying and firing cracks. Sharp internal corners, abrupt section changes, and trapped thick junctions concentrate stress. The part cracks at the exact place where the CAD looked cleanest.
- Release failure (sticking / tearing). Zero draft, soft undercuts and textured vertical walls lock the green body into the plaster mold. The piece either tears on demold or the mold is destroyed extracting it.
- Dimensional mismatch after firing. Lids, threads, stackable feet, silicone lids and coaster recesses designed at nominal size will be 19%–22% too small after the kiln. Mating features must be compensated, not scaled blindly.
2. Shrinkage Data You Must Design Around (Verified Numbers)
This is the single most consequential number in ceramic DFM. Our production data for Dehua bodies:
| Body | Firing temperature | Drying shrinkage | Firing (vitrification) shrinkage | Total linear shrinkage |
|---|---|---|---|---|
| High-Fire White Porcelain (Dehua) | 1310°C | 6% – 8% | 13% – 15% | 19% – 22% |
| Mid-Fire Stoneware | 1260°C – 1280°C | 5% – 7% | 11% – 12% | 16% – 18% |
Two practical consequences:
- A mug designed at 90 mm green height in high-fire porcelain lands at roughly 70–73 mm after firing. If your target is 90 mm fired, the master model must be built at about 111–115 mm.
- Shrinkage is not perfectly isotropic. Slip-cast walls shrink slightly more across the thickness than along the length because the mold extracts water from one face first. Expect 0.5%–1.5% directional variance, which is why we fire a 100 mm shrinkage bar from every new body lot and adjust the master mold rather than trusting a catalogue value.
Body choice changes the whole tolerance chain — see our comparison of high-fire porcelain at 1310°C vs. mid-fire stoneware for custom cafe mugs before locking a fired dimension.
2.1 Scaling Compensation Formula
Compensation is a uniform inverse scale applied to the fired target model to produce the master/green model:
Scale factor = 1 / (1 − S), where S is total linear shrinkage.
| Total shrinkage S | Scale factor | 90.0 mm fired target → master size |
|---|---|---|
| 16% | 1.190 | 107.1 mm |
| 17% | 1.205 | 108.4 mm |
| 18% | 1.220 | 109.8 mm |
| 19% | 1.235 | 111.1 mm |
| 20% | 1.250 | 112.5 mm |
| 21% | 1.266 | 113.9 mm |
| 22% | 1.282 | 115.4 mm |
2.2 How to Apply the Scale in Rhino / SolidWorks / Fusion 360
Rhino: keep the client-facing model at fired size and work on a separate layer or file for the master. Use Scale3D with the model centroid or a defined datum as the base point, and set the scale factor to 1/(1−S). Never scale with “Copy=No” on the only file — keep both states. Record the factor in the file name (e.g. MUG-1140_master_x1.250) so the mold shop cannot use the wrong version.
SolidWorks: use Insert > Features > Scale with uniform scaling about the centroid, driven by a global variable or equation (for example “ScaleFactor” = 1.25). Because it is a feature in the tree, you can suppress it to return to fired size instantly and re-export the client view.
Fusion 360: use Modify > Scale, Uniform, with the body origin as the point, and drive the factor from a user parameter. Also verify that fillets and shell thickness survive the scale — uniform scaling multiplies wall thickness too, so a 3.6 mm wall becomes 4.5 mm at 1.25×, which is usually exactly what you want. If you compensated only one axis, re-check fillets manually.
Critical rule: compensate the model, never the drawing. The 2D drawing must state both sizes — fired target ±tolerance, and master size with the applied factor — or the first article inspection will be measured against the wrong reference.
3. Slip Casting vs. Roller Forming: Two Different CAD Problems
These are not interchangeable processes with different costs. They impose different geometric rules, and choosing the wrong one for a shape is the most expensive mistake in ceramic OEM.
| DFM dimension | Slip Casting (水泥注浆成型) | Roller Forming / Jiggering (滚压成型) |
|---|---|---|
| Geometric freedom | Very high. Free-form organic sculpture, 3D relief, Tiki mugs, animal and character mugs, hollow handles, asymmetric profiles and sculpted lids are all routine. Multi-part molds release true undercuts. | Strictly axisymmetric. Circular plates, standard round cups, round bowls, conical or bell profiles. Any non-round section, handle, or sculptural relief must be added as a separate cast or hand-applied part. |
| Mold format | Multi-piece plaster absorption mold, typically 2–4 parts (up to 6 for complex sculpture), with keys, straps and a pour gate. Each mold produces a limited number of cycles before the plaster saturates. | Single-cavity plaster mold (or plaster head/jigger profile) plus a rotating metal or plaster forming head/profiler that presses the clay against the spinning mold. |
| Clay body & density | Liquid slip at roughly 1.65–1.80 g/cm³, deflocculated, cast by capillary water absorption into the plaster. Density depends on casting time and wall build-up. | High-plasticity vacuum-pugged clay slugs (de-aired), mechanically pressed and thinned by the roller. Higher and more uniform green density, fewer pinholes, better mechanical strength. |
| Wall thickness control | Controlled by dwell time, not by the model. Achievable 3.5–6 mm, tolerance typically ±0.4–0.6 mm. Variation between mold halves is normal; wall must be designed with margin. | Controlled by the gap between profiler and mold — highly repeatable, tolerance typically ±0.2–0.3 mm. Excellent for thin, even rims and tight fired capacities. |
| Production rhythm | Slow: pour, dwell, drain, set, demold, fettle. Labor-heavy, batch-based, mold-bound. Best for low-to-mid volume and high complexity (economical from 500 pcs). | Fast: seconds per piece on a turntable, one operator per station. Lowest unit cost at volume for round ware; tooling amortizes quickly above a few thousand pieces. |
| Typical applications | Character mugs, sculptural vessels, relief-tile patterns, hollow handles, hotel amenity sets with complex silhouettes. | Standard cafe mugs, plates, bowls, ramekins, stackable dinnerware, high-volume promotional drinkware. |
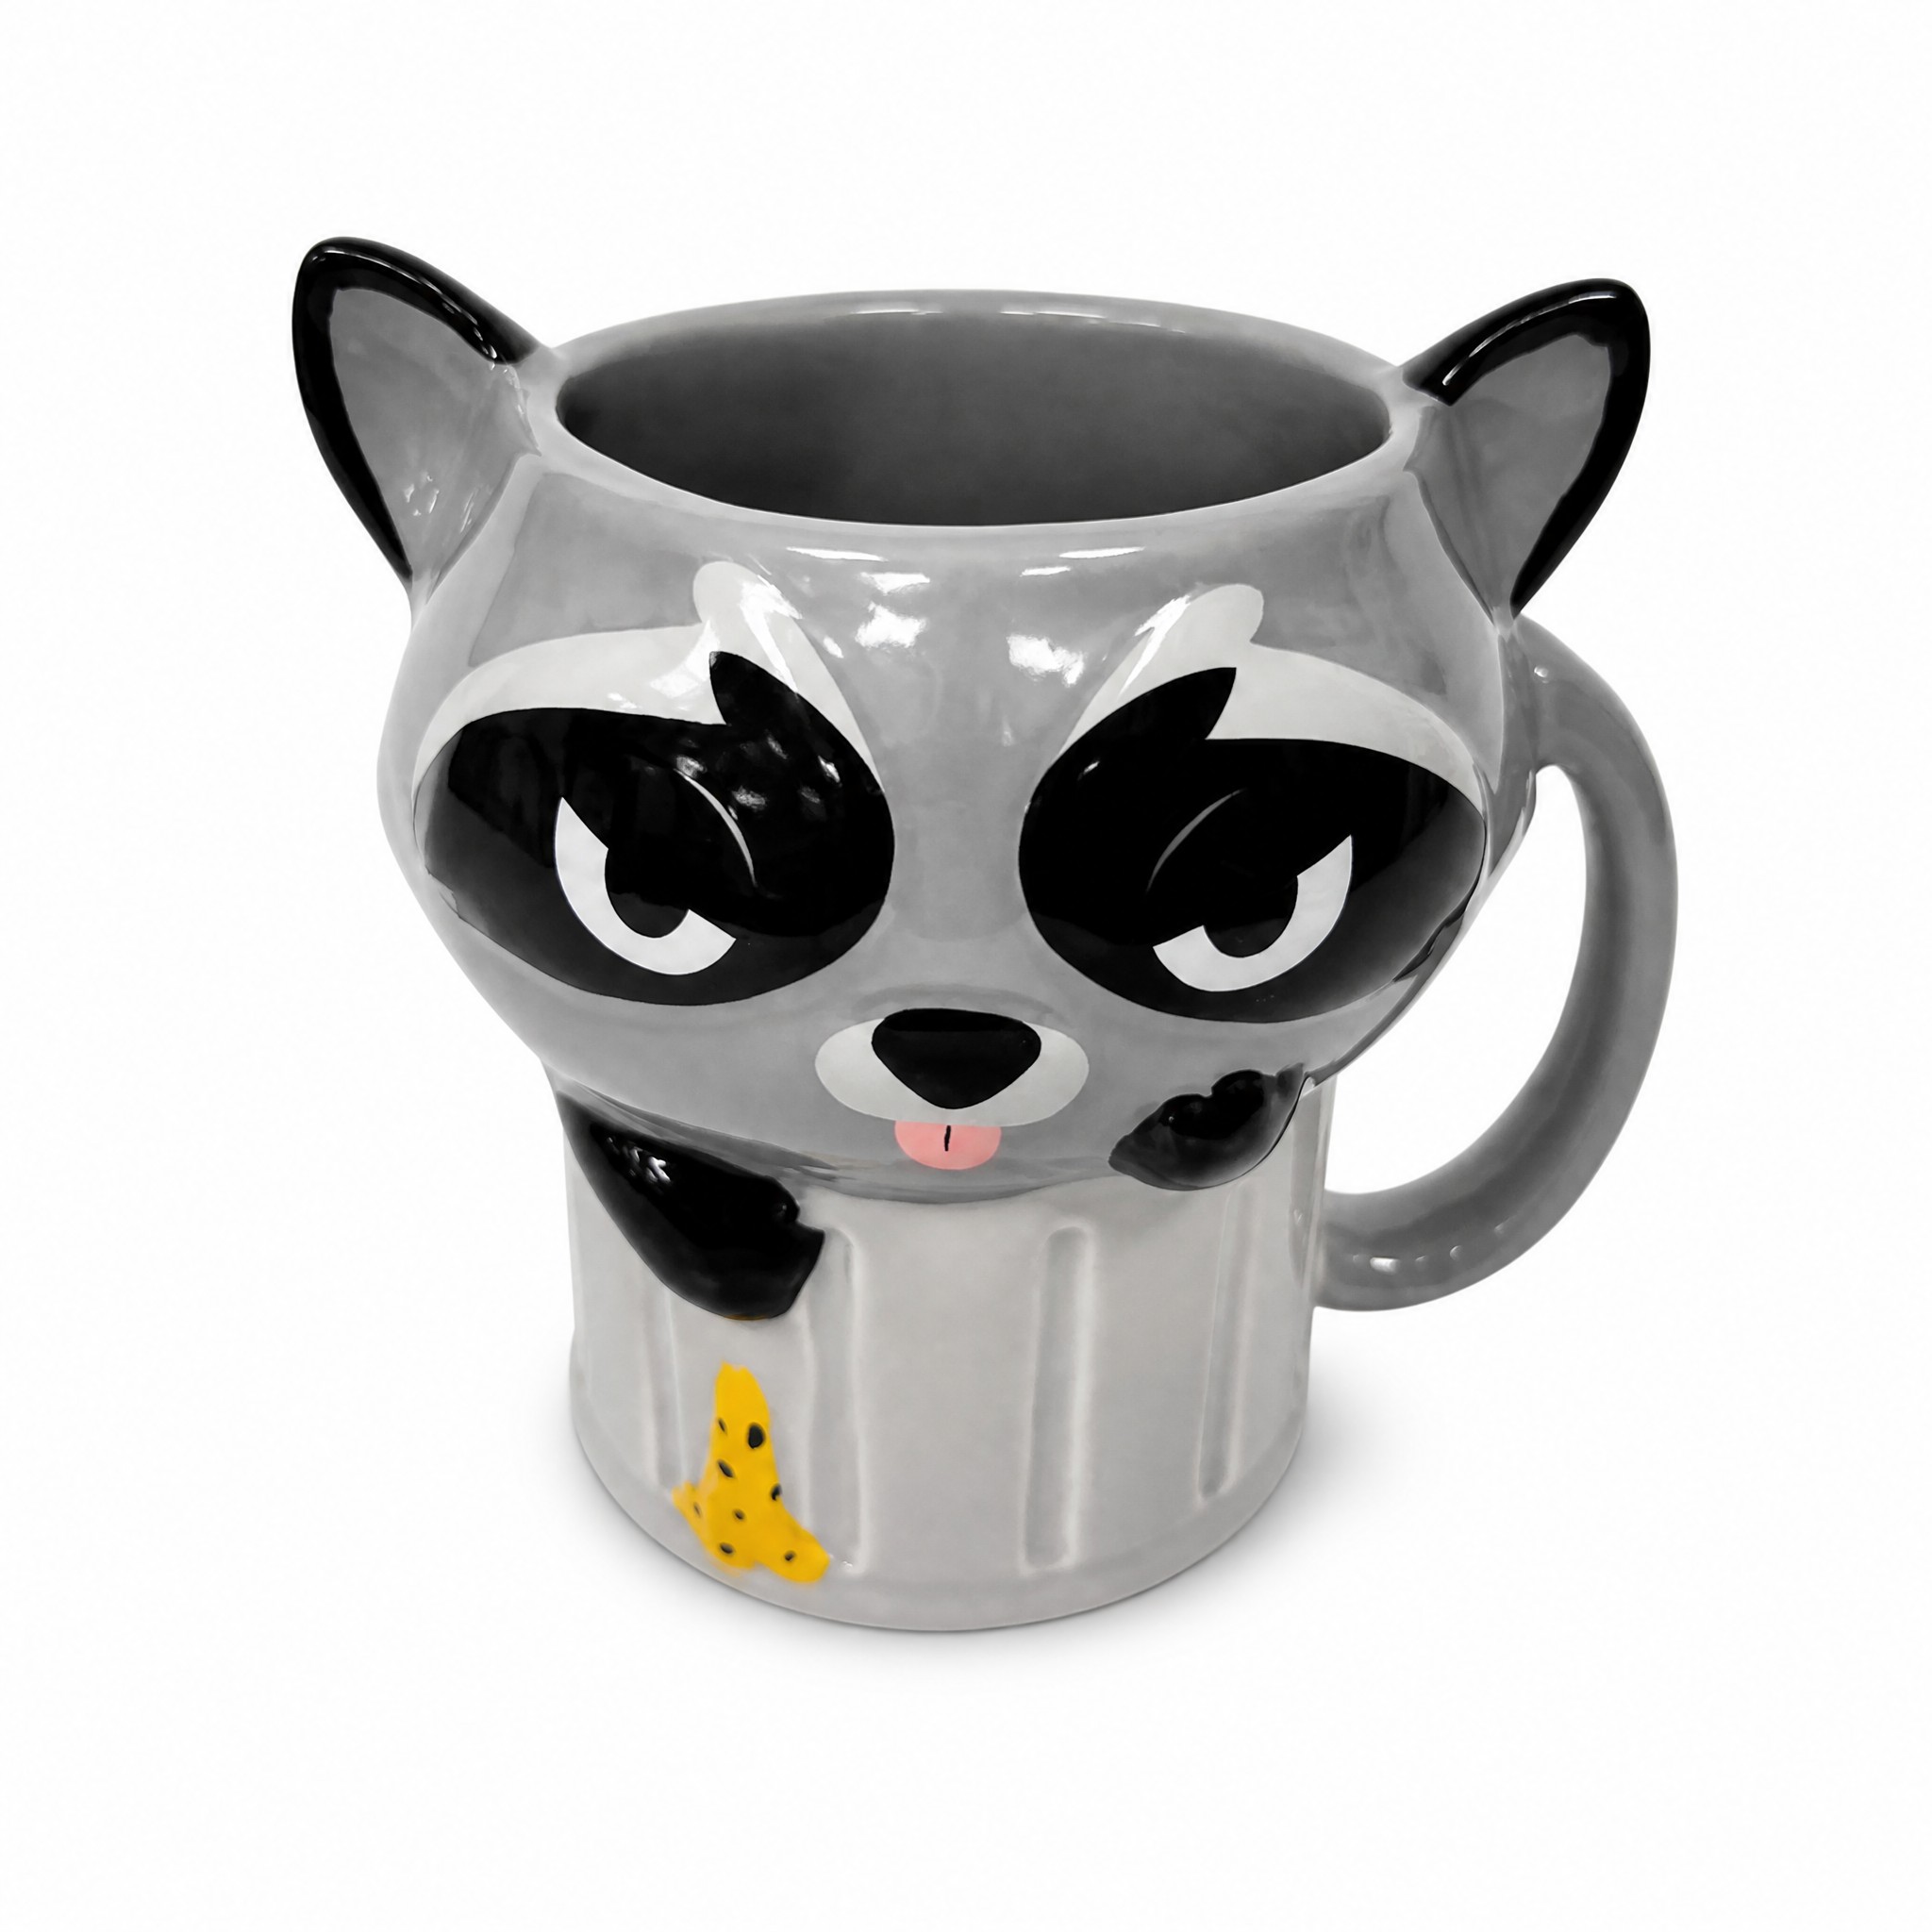
If your design is a sculpted animal form — the kind of work we produce as a 3D sculptural cat & raccoon ceramic mug — slip casting is the only viable route and the CAD must be built for a 2–4 part mold from the first sketch. If it is a 350 ml round latte cup, roller forming will beat slip casting on unit price every time, but the model must be a clean solid of revolution with a separately designed handle.
4. The Five Core Ceramic DFM Rules
Rule 1 — Draft angle: 2°–3° minimum, inside and outside
The green body is soft and wet when it leaves the mold; it has almost no green strength in shear. Apply a minimum of 2° per side on all vertical walls, and 3° on deep female cavities and cores (depth-to-width ratio above 1.5:1). Textured or relief surfaces need 3°–5° because the plaster grips mechanically. Zero-draft cosmetic walls are the number one cause of torn rims. For roller forming, the mold cavity draft can be smaller (1°–2°) because release is axial and assisted by the spinning motion.
Rule 2 — Wall thickness: the 4.5–6.0 mm golden band
Target 4.5 mm to 6.0 mm for the main body wall. Below 4.0 mm, slip casting becomes unreliable and the fired piece chips easily; above 7 mm, drying time doubles and the risk of differential-shrinkage cracking climbs steeply. Keep thickness variation under 2:1 across the part and blend every transition with a radius of at least 1.5–3 mm. A solid, heavy base is a design error: core it or step it, and never let a thick mass sit under a thin wall.
Rule 3 — Parting line placement and undercut avoidance
Place the parting line on the least visible plane, ideally a flat or a designed bead/groove that hides the seam. Two-piece molds handle single-axis undercuts only if the undercut is shallow and radiused; genuine re-entrant geometry requires a 3rd or 4th mold part, which raises tooling cost and cycle time — quantified in our ceramic OEM mold cost breakdown. Design snap features, barbed inserts and dovetail joints out of the green body; post-firing assembly or a silicone/wood add-on is cheaper than a 5-part plaster mold.
Rule 4 — Hollow handles: drain hole and air vent are mandatory
A hollow handle cast as part of the body needs a slip drain/return hole of 4–6 mm at the lowest point and an air-vent hole at the highest point, so slip can drain and air can escape without trapping a pocket. Trapped slip becomes a solid lump that cracks the handle at firing; a sealed void becomes a pressure vessel that blows out. Minimum internal cavity should be 5 mm across, walls 4–5 mm, and the drain hole must be positioned so it can be cleaned and, if required, plugged with a matching glaze-friendly detail.
Rule 5 — Design mating features on the fired dimension
Lids, threads, stacking rings, coaster recesses and silicone-lid grooves must be designed against the fired size and given ceramic-appropriate clearance: 0.8–1.5 mm radial clearance for a lid seat, and never a hard interference fit. Threads are possible but should be coarse (2–3 mm pitch) with rounded crests; fine threads will not survive 20% shrinkage scatter. Specify tolerances as ±0.5 mm or ±1.5% on critical fired dimensions, whichever is larger, and mark every critical dimension on the drawing.
5. File Formats We Need for a Clean DFM Review
| Format | Use it for | Notes |
|---|---|---|
| STEP / STP (AP214 or AP242) | Primary deliverable | Parametric solid, best for mold design, toolpath and CMM. One body per part; no surfaces-only shells; units declared in mm. |
| IGES | Legacy / compatibility | Acceptable fallback when STEP export fails. Expect trimmed-surface gaps; we will heal them and report. |
| STL | Sculptural / relief review | High resolution only: chord tolerance 0.01 mm, angular 5°. Watertight, manifold, single shell. Not accepted as the sole source for mold cutting. |
| 2D drawing (PDF / DWG) | Inspection & approval | Critical dimensions, fired target, tolerances, parting-line direction, gate and drain-hole callouts, glaze boundary. |
| Not accepted | — | .skp, .obj, low-poly meshes, non-manifold or self-intersecting geometry, models already scaled without a stated factor, and files with no dimension reference. |
Send STEP plus drawing and we can usually complete the review without a single clarifying email, then move into master-mold cutting — the workflow we document in the anatomy of rapid ceramic prototyping: from 3D CAD to master mold in 7 days.
6. Pre-Submission Self-Check
- Draft angles: 2° minimum everywhere, 3° on deep cavities — verified.
- Wall thickness 4.5–6.0 mm, no section ratio above 2:1, all transitions radiused.
- Shrinkage factor applied (1.19–1.28), stated in the file name and on the drawing.
- Parting line defined by you, not left to the mold maker.
- Hollow handles: drain hole plus vent hole, no sealed volumes anywhere in the body.
- Lids and mating parts checked at fired size with ceramic clearance.
- Process selected deliberately: slip casting for sculpture and asymmetry, roller forming for axisymmetric volume.
Send Us Your STEP File — Get a DFM Verdict in 24 Hours
Upload your STEP, STL and drawing to our RFQ desk and our engineering team will return a written manufacturability assessment within one working day: draft-angle and wall-thickness audit, parting-line proposal, recommended process (slip casting vs. roller forming), shrinkage factor for your chosen body, mold part count, and a firm piece price with tooling separated out.
Dehua Fugu Ceramics — source factory, not a trading company. In-house mold shop, in-house kilns at 1310°C, Low MOQ 500 pcs, full DFM support from first sketch to shipped pallet.
Submit your 3D files for a 24-hour DFM review & quote →
Or email drawings directly to [email protected] — we reply within one business day.